Product Descriptions
Case Study Methodology
Dr. BOY is internationally recognized in the small and medium-tonnage injection molding segment, particularly for applications requiring technical plastics, high dimensional accuracy, complex geometries, and demanding process conditions.
This case study compilation is based on real industrial production examples manufactured on various Dr. BOY injection molding machine models. The objective is not only to highlight machine capabilities, but also to demonstrate how material selection, mold design, cycle times, cavity layouts, and process challenges are successfully managed using Dr. BOY technology.
Case Study 1 - High-Precision Micro Technical Components
Application Description
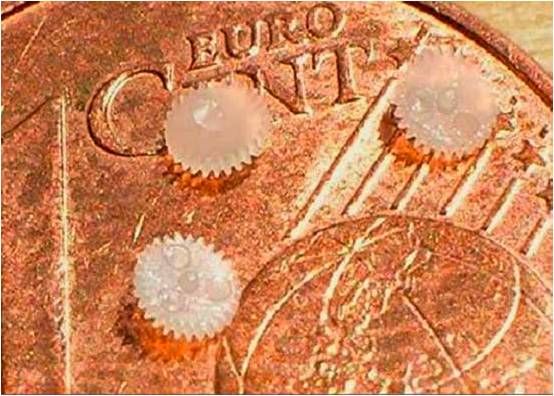
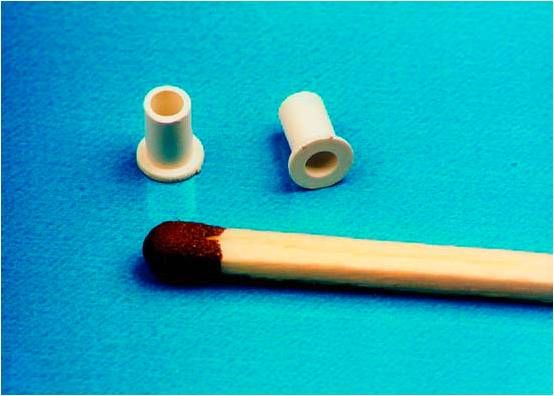
Micro technical components made from PA6 and POM, used in electronic and mechanical sub-assemblies. These parts require extremely tight tolerances and have very low individual weights.
Technical Data
Machine models: BOY 12 A, BOY 22 A, BOY 22 M
Screw diameters: 14 mm - 18 mm
Part weights: 0.025 g - 0.56 g
Shot weights: 1.15 g - 7.8 g
Cycle times: 8.2 s - 15.5 s
Number of cavities: 1 - 4
Process Challenges
Extremely low shot volumes
Thin walls and precision mating surfaces
Zero tolerance for warpage or deformation
Dr. BOY Advantage
High specific injection pressure, stable plasticizing behavior, and precise injection control ensured excellent shot-to-shot repeatability and consistent part weights throughout production.
Case Study 2 - Glass-Fiber-Reinforced Technical Parts
Application Description
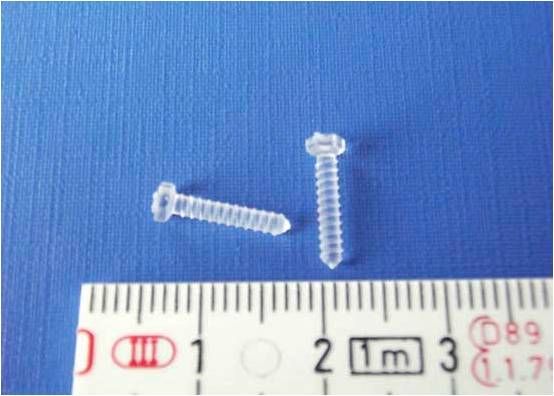
Technical components produced from PA 6 and PA 6.6 with 30-50 percent glass fiber reinforcement, designed for applications requiring high mechanical strength, rigidity, and thermal stability.
Technical Data
Materials: PA 6 GF30, PA 6.6 GF30, PA 6 GF50
Machine models: BOY 22 M, BOY 55 A, BOY 90 A
Screw diameters: 18 mm - 48 mm
Part weights: 0.13 g - 181.3 g
Cycle times: 7.2 s - 36 s
Number of cavities: 1 - 4
Process Challenges
Increased wear due to high glass fiber content
Varying wall thicknesses
Long flow paths and warpage risk
Dr. BOY Advantage
Robust clamping units, high injection forces, and finely adjustable speed and pressure profiles enabled stable processing of glass-fiber-reinforced materials while maintaining surface quality and dimensional accuracy.
Case Study 3 - Thin-Wall and Complex Geometry Components
Application Description
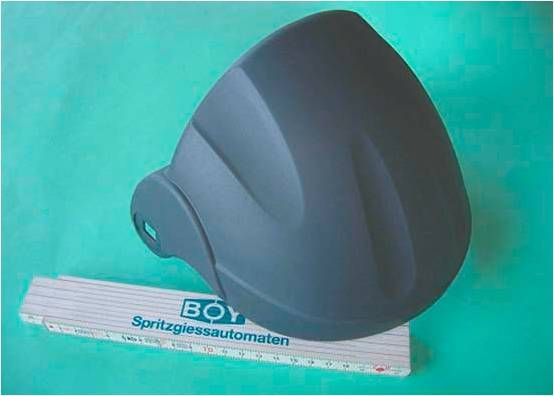
ABS and PBT technical housings and carrier parts featuring multiple clips, holes, ribs, and thin-wall sections.
Technical Data
Machine models: BOY 22 M, BOY 30 M, BOY 90 M
Screw diameters: 18 mm - 42 mm
Part weights: 0.12 g - 121.4 g
Projected area: above 300 cm²
Cycle times: 8 s - 25 s
Process Challenges
High flow-length-to-wall-thickness ratios
High surface quality requirements
Strict dimensional stability
Dr. BOY Advantage
High injection speed capability and excellent process stability allowed consistent production of thin-wall, complex parts with low scrap rates.
Case Study 4 - Multi-Cavity High-Volume Production
Application Description
Small ABS parts designed for mass production, such as pen clips and similar components.
Technical Data
Machine model: BOY 90 M
Screw diameter: 36 mm
Number of cavities: 32 - 64
Part weights: 0.53 g - 0.63 g
Cycle times: 13 s - 14.8 s
Process Challenges
Very high cavity count
Long-term process repeatability
Stable quality over millions of cycles
Dr. BOY Advantage
High mechanical rigidity and long-term process stability ensured consistent quality throughout extended high-volume production runs.
Case Study 5 - Special Processes: Gas-Assisted and IMD Applications
Application Description
Gas-assisted injection molding (GIT) for thick-section parts without sink marks
In-Mold Decoration (IMD) for parts with integrated decorative surfaces
Technical Data
Machine models: BOY 50 A, BOY 90 A
Part weights: 5.65 g - 39.9 g
Cycle times: 9.7 s - 35 s
Process Challenges
Sink mark control
Maintaining decorative surface integrity
Integration of additional process technologies
Dr. BOY Advantage
High control precision and flexible integration options allowed advanced processes to be seamlessly combined with standard injection molding operations.
Overall Evaluation - Results from Dr. BOY Case Studies
The results obtained from these case studies clearly demonstrate that Dr. BOY injection molding machines provide strong and reliable solutions in the following areas:
Wide application range from micro parts to high shot weights
Tight dimensional tolerances and superior surface quality
Reliable processing of glass-fiber-reinforced and demanding engineering plastics
Short cycle times and high process repeatability
Long-term stability in serial production
Conclusion - Why Choose Dr. BOY for Technical Parts?
Dr. BOY injection molding machines offer more than just equipment; they provide process reliability, consistent quality, and engineered solutions for technical plastic parts production. These real industrial case studies clearly illustrate why Dr. BOY is trusted for applications ranging from micro-precision components to robust technical parts produced in high volumes.