Product Descriptions
Case Study Approach in Caps and Closures Injection Molding
Caps and closure systems are among the most productivity-driven product groups in injection molding for the packaging industry. These applications require extremely short cycle times, high cavity counts, very low part weights, and flawless reproduction of functional details. Features such as tamper-evident rings, flip-top mechanisms, screw threads, and sealing surfaces significantly increase the importance of process stability.
Key requirements for injection molding machines used in cap production include:
- Balanced filling in high-cavity molds
- Repeatable quality at very short cycle times
- Full compatibility with hot runner systems
- Stable operation with unscrewing systems, in-mold closing, and integrated mechanisms
- Mechanical and thermal stability during continuous serial production
Dr. BOY injection molding machines provide a powerful production platform for caps and closures thanks to their compact design and precise injection characteristics.
Case Study 1 - HDPE Dropper Production | 24 Cavities
Application Description
Production of very small and lightweight HDPE droppers used in pharmaceutical and chemical packaging. Due to the high cavity count and extremely low part weight, injection balance is critical.
Technical Data
Part type: Dropper
Material: HDPE
Part weight: 0.45 g
Shot weight: 11.0 g
Machine: BOY 22 M
Screw diameter: 22 mm
Cycle time: 17 s
Number of cavities: 24
Runner system: Hot runner (hot edge), 6 hot runner nozzles with 4 gates each
Process Challenge
Simultaneous filling of 24 cavities, stable shot control despite low part weight, and flash-free production.
Dr. BOY Advantage
Precise injection and holding pressure control ensured consistent weight and geometry across all cavities.
Case Study 2 - LDPE Tamper-Evident Ring (Safety Seal Ring)
Application Description
Production of a tamper-evident ring with extremely thin connection bridges, used in bottle and cap systems.
Technical Data
Part type: Tamper-evident ring
Material: LDPE
Part weight: 0.5 g
Shot weight: 4.1 g
Machine: BOY 30 M
Screw diameter: 24 mm
Cycle time: 5.8 s
Number of cavities: 8
Runner system: Hot runner
Process Challenge
Precise control of break points and stable material flow through very thin sections.
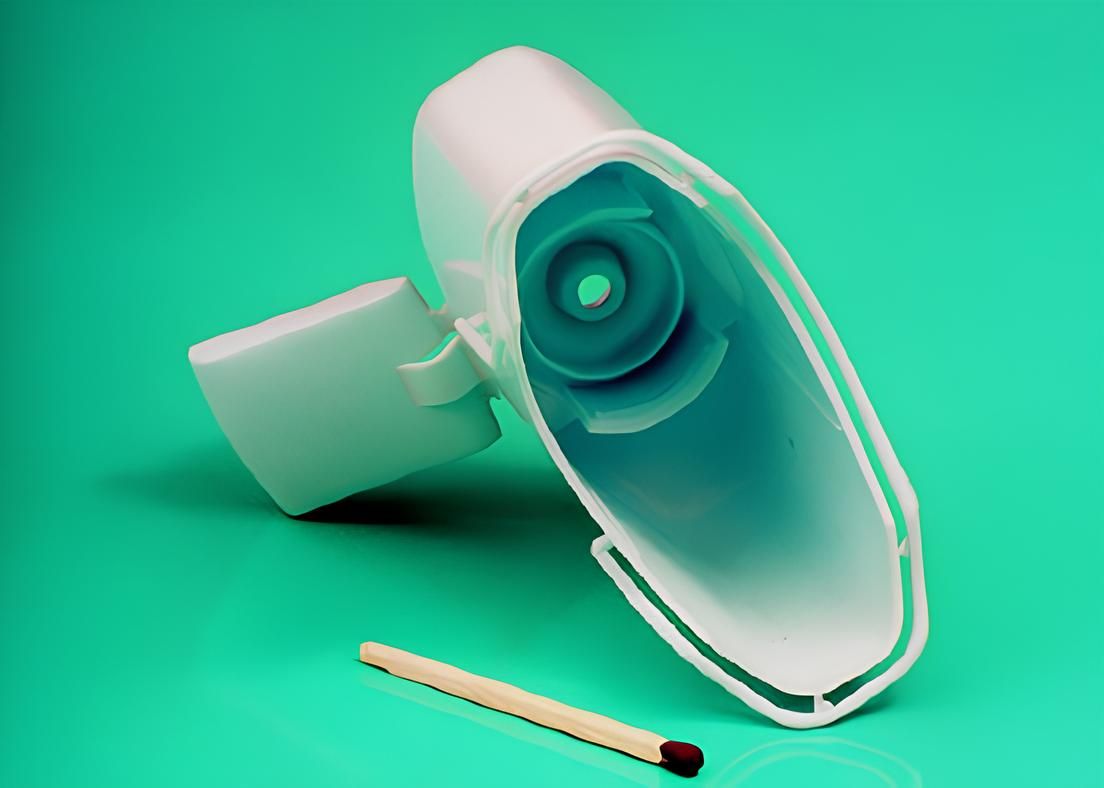
Case Study 3 - PP Flip-Top Cap
Application Description
Production of a flip-top cap used in cosmetics and personal care packaging. The cap is closed inside the mold before ejection.
Technical Data
Part type: Flip-top cap
Material: PP
Part weight: 2.85 g
Shot weight: 17.7 g
Machine: BOY 35 M
Screw diameter: 28 mm
Cycle time: 14 s
Number of cavities: 4
Runner system: Sprue gate with distributor and tunnel gates
Process Challenge
Durability of the hinge and synchronized operation of the in-mold closing mechanism.
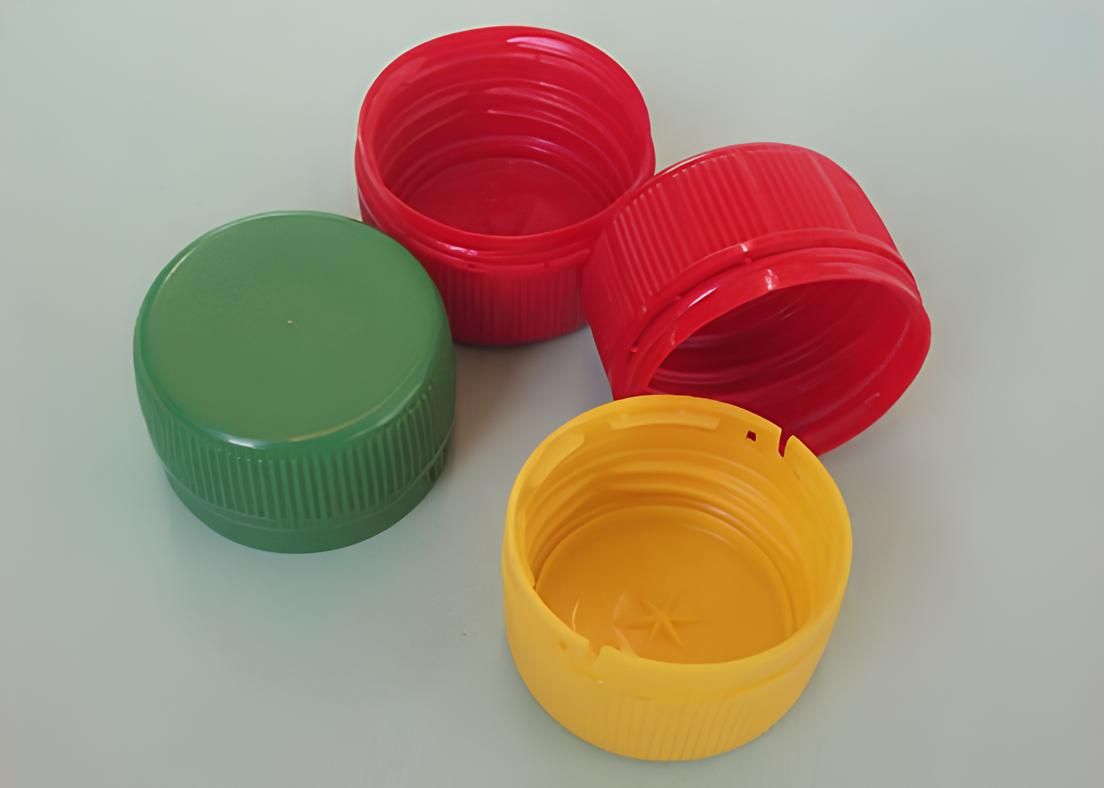
Case Study 4 - 28 mm HDPE Screw Cap | 12 Cavities
Application Description
Production of a 28 mm screw cap widely used in beverage and food packaging.
Technical Data
Part type: 28 mm screw cap
Material: HDPE
Part weight: 2.8 g
Shot weight: 33.6 g
Machine: BOY 50 M
Screw diameter: 38 mm
Cycle time: 10.2 s
Number of cavities: 12
Runner system: Hot runner with point gating
Process Challenge
Efficient cooling to achieve short cycle times and damage-free demolding of screw threads.
Case Study 5 - HDPE Canister Cap
Application Description
Production of a heavy-duty HDPE canister cap for industrial packaging applications.
Technical Data
Part type: Canister cap
Material: HDPE
Part weight: 12.05 g
Shot weight: 48.2 g
Machine: BOY 55 M
Screw diameter: 38 mm
Cycle time: 12 s
Number of cavities: 4
Runner system: Hot runner
Case Study 6 - Special PP Cap for the Chemical Industry
Application Description
Production of a PP screw cap designed for chemical industry applications with enhanced sealing and mechanical strength requirements.
Technical Data
Part type: Screw cap
Material: PP
Part weight: 8.86 g
Shot weight: 35.5 g
Machine: BOY 55 A
Screw diameter: 32 mm
Cycle time: 17 s
Number of cavities: 4
Runner system: Hot runner
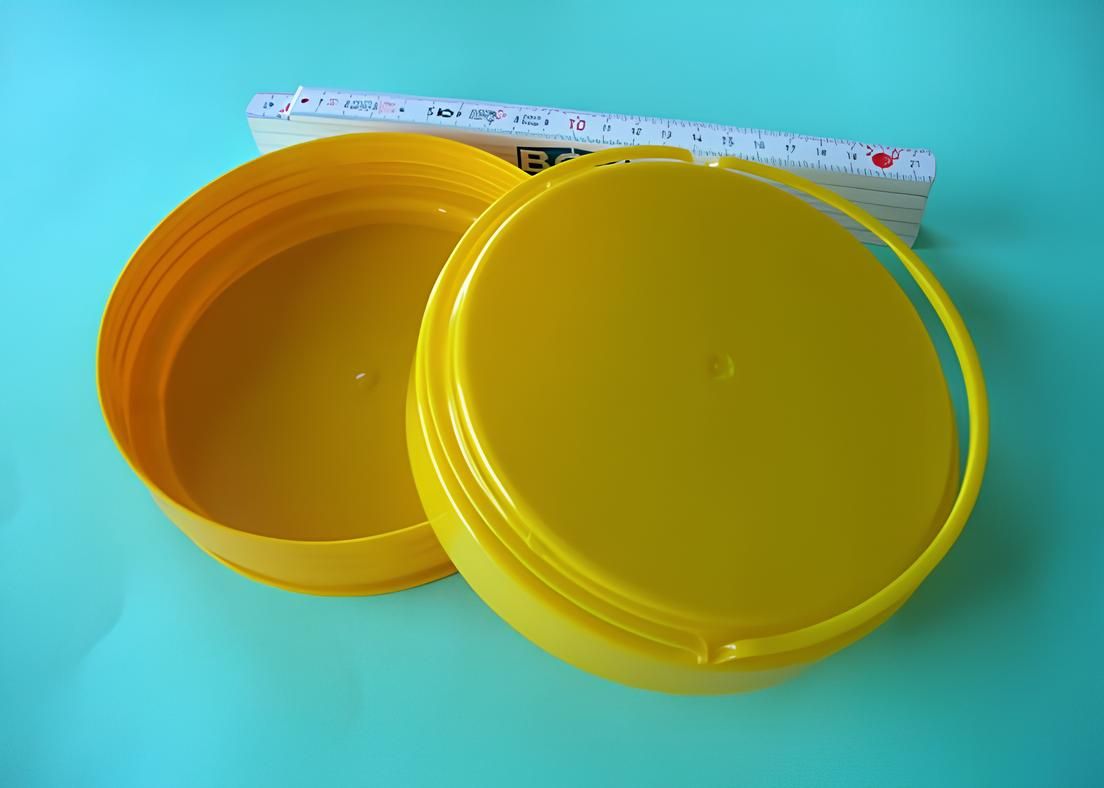
Case Study 7 - Canister Cap with Integrated Carrying Handle
Application Description
Production of a large PP canister cap with an integrated carrying handle molded as part of the component.
Technical Data
Part type: Canister cap with handle
Material: PP
Part weight: 40.8 g
Shot weight: 40.8 g
Machine: BOY 55 M
Screw diameter: 32 mm
Cycle time: 14 s
Number of cavities: 1
Runner system: Heated sprue bushing
Case Study 8 - HDPE Flip-Top Cap with Automatic In-Mold Closing
Application Description
Production of a flip-top cap that is automatically closed inside the mold during the molding cycle.
Technical Data
Part type: Flip-top cap
Material: HDPE
Part weight: 2.85 g
Shot weight: 17.7 g
Machine: BOY 55 A
Screw diameter: 32 mm
Cycle time: 18 s
Number of cavities: 4
Runner system: Runner distributor
Case Study 9 - HDPE Cosmetic Bottle Cap | 8 Cavities
Application Description
Production of an HDPE cosmetic bottle cap that locks inside the mold.
Technical Data
Part type: Cosmetic bottle cap
Material: HDPE
Part weight: 10.21 g
Shot weight: 81.68 g
Machine: BOY 80 T2
Screw diameter: 42 mm
Cycle time: 15 s
Number of cavities: 8
Runner system: Hot runner
Overall Evaluation - Results from Caps Injection Case Studies
These caps and closures case studies clearly demonstrate the strengths of Dr. BOY injection molding machines in the following areas:
- Balanced filling in high-cavity cap molds
- Stable serial production at extremely short cycle times
- Full compatibility with hot runner and point-gate systems
- Functional reliability of flip-top, tamper-evident, and screw-threaded caps
- Broad application range in food, cosmetic, and industrial packaging
Conclusion - Why Choose Dr. BOY for Caps and Closures Injection Applications?
Dr. BOY injection molding machines offer more than high-speed solutions for cap production. They provide a robust manufacturing platform delivering process stability at high cavity counts, low scrap rates, and long-term production reliability. These real industrial case studies clearly demonstrate why Dr. BOY is a trusted choice for caps and closure systems manufacturing.