Product Descriptions
Case Study Approach in Micro Injection Molding
Dr. BOY is widely regarded as a benchmark manufacturer in the field of micro injection molding. Micro molding represents one of the most demanding disciplines within injection molding, characterized by extremely low shot weights, very narrow processing windows, high specific injection pressures, and the need for exceptionally precise process control.
This case study compilation is based on real industrial production examples manufactured on Dr. BOY injection molding machines. The objective is not merely to present finished parts, but to demonstrate how machine configuration, screw diameter selection, cycle time optimization, cavity layout, and material sensitivity are successfully managed at milligram and even microgram scale.
Case Study 1 - LCP Micro Parts with Minimal Shot Weight
Application Description
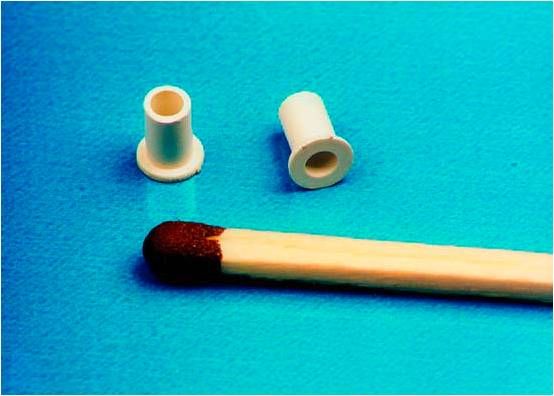
Micro bearing bush components manufactured from LCP (Liquid Crystal Polymer). This application represents one of the most extreme examples of micro injection molding, where the required shot weight approaches the technical limits of conventional injection systems.
Technical Data
Part type: Bearing bush
Material: LCP
Part weight: 0.014 g
Shot weight: 0.207 g
Injection molding machine: BOY 12 A
Screw diameter: 14 mm
Cycle time: 3 s
Number of cavities: 3
Runner system: Hot runner with sub-distributor
Process Challenges
Extremely low part and shot weight
Highly sensitive dosing requirements despite LCP's high flowability
Strict shot-to-shot weight repeatability
Dr. BOY Advantage
High specific injection pressure combined with stable plasticizing behavior enabled consistent part weights at milligram level across continuous production cycles.
Case Study 2 - Thin-Wall Micro Components (0.3 mm Wall Thickness)
Application Description
Pump housing components produced from LCP with a minimum wall thickness of just 0.3 mm, pushing the flow and filling limits of micro injection molding technology.
Technical Data
Material: LCP
Part weight: 0.037 g
Shot weight: 0.280 g
Injection molding machine: BOY 12 A
Screw diameter: 14 mm
Cycle time: 8 s
Number of cavities: 1
Runner system: Heated nozzle, sub-runner, and tunnel gate
Process Challenges
Extremely high flow-length-to-wall-thickness ratio
Risk of premature cooling during filling
Surface integrity and defect-free molding
Dr. BOY Advantage
Precisely controlled injection speed and pressure profiles ensured complete and flash-free filling of thin-wall micro geometries.
Case Study 3 - Thick-Section Micro Parts with Flat Surface Requirements
Application Description
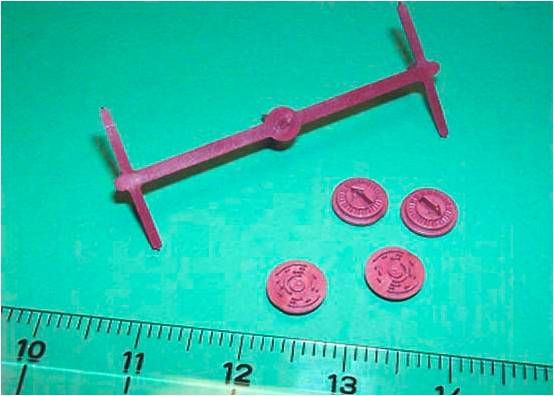
Micro components manufactured from LCP Vectra E131 featuring thick cross-sections while requiring completely flat, sink-free visible surfaces.
Technical Data
Part type: Cam disc
Material: LCP Vectra E131
Part weight: 0.094 g
Shot weight: 1.16 g
Injection molding machine: BOY 12 A
Screw diameter: 14 mm
Cycle time: 9.5 s
Number of cavities: 8
Runner system: Heated hot runner pin
Process Challenges
Sink mark risk in thick sections
Balanced filling across multiple cavities
Dr. BOY Advantage
Stable holding pressure control and highly repeatable process parameters ensured flat surfaces and uniform cavity filling.
Case Study 4 - Medical and Biodegradable Micro Components
Application Description
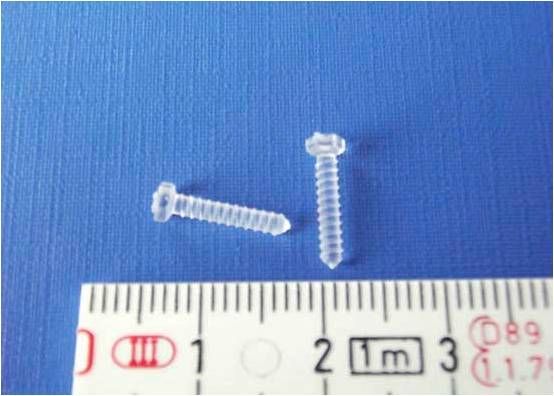
Resorbable implant screws and fixation elements manufactured from Poly-L-Lactide (PLA) and PLA-based biodegradable polymers for medical applications.
Technical Data
Part type: Resorbable implant screw
Material: Poly-L-Lactide
Part weight: 0.033 g
Shot weight: 0.82 g
Injection molding machine: BOY 12 A
Screw diameter: 14 mm
Cycle time: 13 s
Number of cavities: 2
Process Challenges
Extremely expensive and thermally sensitive material
Risk of material degradation
Strict medical tolerance requirements
Dr. BOY Advantage
Short residence times and controlled plasticizing minimized material waste and enabled safe, repeatable production of medical-grade micro components.
Case Study 5 - Micro Gears and Mechanical Precision
Application Description
Micro gears manufactured from POM with extremely small geometrical features, including module 0.07, 27 teeth, and a pitch diameter of 1.89 mm.
Technical Data
Part type: Micro gear
Material: POM
Part weight: < 0.001 g
Shot weight: 0.1 g
Injection molding machine: BOY 12 A
Screw diameter: 12 mm
Cycle time: 6 s
Number of cavities: 2
Mold design: Three-plate mold with heated sprue bushing
Process Challenges
Precise filling of micro gear tooth geometry
Dimensional accuracy and tooth profile integrity
Dr. BOY Advantage
Vibration-free injection behavior and high process repeatability enabled compliance with strict micro-mechanical tolerances.
Overall Evaluation - Results from Dr. BOY Micro Injection Case Studies
These micro injection molding case studies clearly demonstrate that Dr. BOY injection molding machines deliver reliable and robust solutions in the following areas:
Stable production of parts weighing below 0.001 g
Safe processing of demanding materials such as LCP, POM, PFA, PA, and PLA
Very short cycle times ranging from 3 to 14 seconds
High specific injection pressure and exceptional process stability
Outstanding dimensional repeatability in micro geometries
Conclusion - Why Choose Dr. BOY for Micro Injection Applications?
Dr. BOY injection molding machines offer more than just equipment for micro molding; they provide a high-precision process platform specifically engineered for ultra-small, high-value components. These real industrial case studies clearly demonstrate why Dr. BOY is a preferred solution for micro parts, medical components, and micro-mechanical systems where accuracy, repeatability, and process reliability are critical.