Product Descriptions
Machining Oils and Cutting Fluids
Oils and cutting fluids used in machining operations are essential for reducing friction between the cutting tool and workpiece, controlling temperature in the cutting zone, removing chips and protecting machined surfaces.
The correct metalworking fluid can help extend tool life, improve surface quality, increase machining speed and reduce production costs. Incorrect product selection or poor emulsion management may result in tool wear, staining, corrosion, foam, unpleasant odours, bacterial contamination and unstable process conditions.
ACCA machining oils and cutting fluids are developed for turning, milling, drilling, grinding, reaming, broaching, threading, tapping and similar metal-removal operations. The range includes synthetic, semi-synthetic and mineral water-miscible fluids, as well as straight oils, special cutting oils and emulsion-maintenance additives.
Synthetic Metalworking Fluids
Synthetic cutting fluids contain no mineral oil or have a very low oil content. They are particularly suitable for applications requiring high cooling performance, good process visibility and low residue in the machining area.
The ACCA COOLD range provides synthetic solutions for general machining, grinding and hard-metal processing.
COOLD is a synthetic fluid that can replace conventional emulsifiable oils in various metalworking operations. It provides cleaning, antioxidant and microbiological-stability properties, together with lubricating and extreme-pressure additives.
COOLD COBALTO is developed for grinding cobalt-containing hard metals. Its transparent working solution and specialised corrosion inhibitors support process visibility and metal-surface protection.
COOLD R is a synthetic fluid particularly suitable for grinding. It creates a transparent solution and helps protect machine equipment and painted surfaces.
SYNTHETIC CUT is a low-foaming synthetic coolant developed for lapping and grinding ferrous materials and alloy steels. It provides high cooling and cutting performance.
Semi-Synthetic Cutting Fluids
Semi-synthetic metalworking fluids combine synthetic components with a controlled proportion of mineral or synthetic oil. They provide a balance between cooling, lubrication, surface protection and emulsion stability.
The ACCA SINTAX and SEMISINT product families are developed for operations ranging from light machining to high-load applications.
SINTAX C NEW is a semi-synthetic product with high cooling and cleaning performance for light- and medium-duty cutting and grinding operations.
SINTAX BIO HP combines mineral oil, synthetic esters, corrosion inhibitors and extreme-pressure additives. It is developed for demanding machining operations and is free from boron, formaldehyde, chlorine and secondary amines.
SINTAX S-BIOD ECO and SINTAX EP ECO can be used for medium- and heavy-duty operations requiring strong lubrication and extreme-pressure performance. SINTAX EP ECO has a biostable formulation designed to support stability in hard water.
SINTAX FB is a biocide-free semi-synthetic fluid developed for cutting and grinding aluminium, steel and ferrous materials.
SEMISINT BIO M-BFF is designed particularly for demanding operations involving aluminium, copper and yellow alloys. It contains lubricating, corrosion-inhibiting and extreme-pressure additives while being free from formaldehyde, boron and amines.
SEMISINT provides lubrication, cooling and rust protection during medium-duty operations on steel and cast iron.
SEMISINT BIO can be used for turning, milling, drilling and grinding steel, cast iron, aluminium and yellow alloys.
SEMISINT YELLOW is a specialised product designed to help control staining on aluminium, copper, brass and other yellow alloys.
Mineral-Based Emulsions
Mineral-based emulsions are widely used in general machining applications requiring a high level of lubrication. When correctly mixed with water, they combine cooling and lubricating performance.
COOLD EM 160 BIO is a mineral-based fluid designed to support long-term emulsion stability and control mould and bacterial contamination. It is free from boron, sulphur, phosphorus, zinc and free secondary amines.
COOLD EM 160 is a metalworking fluid free from chlorine, formaldehyde and secondary amines. It can be used for general mechanical machining and contains components that support cooling performance and low sludge formation.
Straight Oils and Special Cutting Oils
Straight oils are used without mixing with water. They are preferred for drilling, threading, tapping and heavy machining operations requiring strong lubrication, extreme-pressure resistance and tool protection.
CUTTING OIL is a synthetic cutting oil containing anti-wear and anti-seize additives for drilling, threading and tapping iron, steel and special steels. The aerosol version provides convenient application for maintenance and local machining operations.
CUTTING OIL LC has a lower viscosity and can therefore be applied through automatic spraying systems.
CUTTING ALLUMINIO is a low-viscosity fluid developed for drilling and threading aluminium, copper and light alloys.
CUT LUBE PLUS LP is a synthetic-ester-based product for heavy grinding, drilling and tapping operations. It contains no mineral oil and has low volatility.
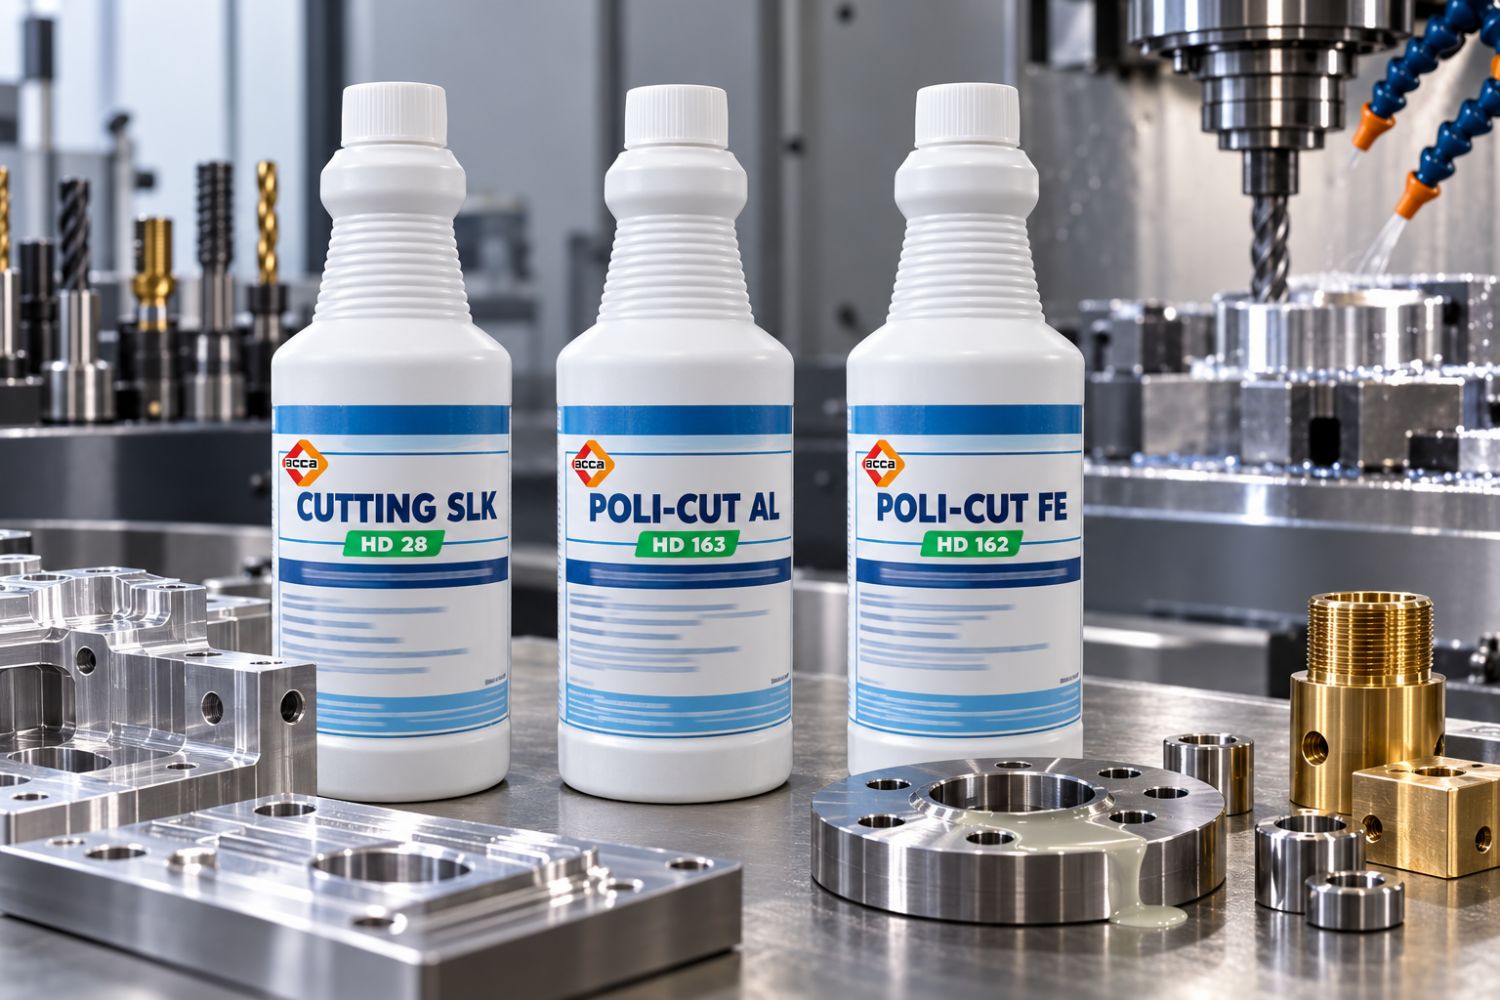
CUTTING SLK is a high-viscosity fluid developed for demanding or high-precision tapping and threading of steel and hard metals.
POLI-CUT AL is intended for aluminium and its alloys, POLI-CUT CU for copper and yellow alloys, and POLI-CUT FE for iron, special steels and cast iron.
LUBRO MIN TO is a mineral-based product for high-speed turning of light and yellow alloys. LUBRO SYNT TO contains synthetic esters and extreme-pressure additives for medium- and heavy-duty turning.
The RAPID range includes cooling and anti-wear fluids for tapping and threading different metals.
Emulsion Maintenance and Process Control
To maintain the performance of water-miscible metalworking fluids, the emulsion must be monitored regularly. Concentration, pH, water hardness, temperature, microbiological loading, tramp-oil content and filtration conditions directly affect fluid life.
EMULCLEAN is a concentrated cleaner designed for metalworking-fluid tanks and circulation systems. In suitable applications, it can support system cleaning without completely interrupting production.
HD 160/1 is an additive that helps control unpleasant odours and microbiological degradation in mineral and semi-synthetic emulsions.
HD 29/1 is developed for decontamination and odour control in synthetic metalworking fluids.
STEP is a water-miscible additive formulated to increase the extreme-pressure performance of semi-synthetic and mineral fluids.
When preparing an emulsion, the concentrate should be added slowly and steadily to the water. Adding water directly to the concentrate may negatively affect emulsion stability. Concentration should be checked regularly with a refractometer, and tramp oils should be removed using suitable skimming or separation equipment.
Main Application Areas
- Turning
- Milling
- Drilling and deep-hole drilling
- Tapping and threading
- Grinding and precision grinding
- Reaming
- Broaching
- Lapping
- Cutting and sawing
- CNC machining centres
- Automatic and multi-spindle machines
- Iron and steel machining
- Cast-iron machining
- Aluminium and light-alloy machining
- Copper, brass and yellow-alloy machining
- Grinding of hard metals and cobalt-containing materials
Main Benefits
- Helps control temperature in the cutting zone
- Reduces friction between the tool and workpiece
- Helps limit tool wear and built-up edge
- Supports the surface quality of machined components
- Facilitates chip removal from the cutting area
- Helps protect workpieces and machine tools against corrosion
- Supports stable machining speeds and process conditions
- Helps reduce foam, fumes and residue when the correct product is selected
- Contributes to longer emulsion life and reduced fluid consumption
- Provides synthetic, semi-synthetic, mineral and straight-oil options for different metals and operations
Product Selection Considerations
Cutting-fluid selection should consider the workpiece metal, severity of the operation, tool material, cutting speed, required surface quality, machine filtration system, water hardness and subsequent manufacturing stages.
Non-staining products should be selected for aluminium and yellow alloys. Extreme-pressure and anti-wear additives become more important when machining steel and hard metals. Grinding operations generally require high cooling, low foam, effective filtration and low residue.
ACCA technical data sheets, safety data sheets and actual process conditions should be reviewed when determining the correct product and working concentration. Regular emulsion analysis and recordkeeping help maintain product performance and process stability.