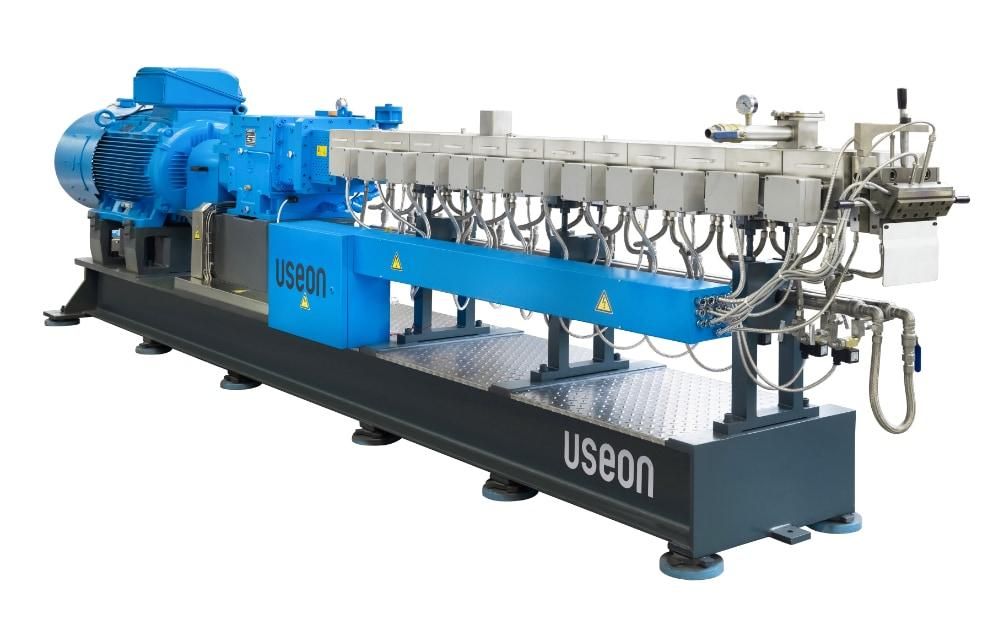
Does Higher Screw Speed Improve Dispersion in Twin-Screw Extruders?
Does Higher Screw Speed Improve Dispersion in Twin-Screw Extruders?
USEON examines how screw speed affects dispersion quality in twin-screw extrusion and highlights the importance of selecting optimal processing conditions for consistent product quality.
Achieving homogeneous mixing is essential in plastic compounding, masterbatch production, and the processing of polymers containing pigments, fillers, and additives.
When manufacturers encounter pigment agglomerates, poor filler dispersion, or inconsistent color distribution, increasing screw speed is often one of the first adjustments considered.
However, according to a technical article published by USEON, higher screw speed does not necessarily result in better dispersion. While increasing screw speed may improve mixing performance in certain applications, it can also raise melt temperature and negatively affect material properties.
Understanding Dispersive and Distributive Mixing
Twin-screw extrusion involves two important mixing mechanisms:
Dispersive mixing: The mechanical breakdown of pigment and filler agglomerates through sufficient stress within the polymer melt.
Distributive mixing: The uniform distribution of components throughout the polymer matrix.
Both mechanisms are essential for achieving consistent product quality. However, improving one does not automatically guarantee improvement in the other.
How Does Screw Speed Affect Dispersion?
Increasing screw speed generally increases the local shear rate in certain sections of the extruder, particularly within kneading and mixing zones.
This additional mechanical action may help break down pigment and filler agglomerates, provided that the materials have been sufficiently melted and wetted.
However, higher screw speed also influences several processing parameters:
Shear rate and stress: Changes in the mechanical forces acting on the material.
Melt temperature: Increased mechanical energy may lead to additional heat generation.
Melt viscosity: Changes due to shear-thinning behavior and temperature variations.
Fill level: Changes in material distribution within the screw channels.
Residence time: Changes in how long the material remains inside the extruder.
For example, increasing screw speed from 300 rpm to 600 rpm may significantly increase local shear rates. However, this does not mean that shear stress or dispersion efficiency will automatically double.
Because polymer melts typically exhibit non-Newtonian behavior, viscosity can decrease as shear rate and temperature increase.
The actual dispersion result therefore depends on the interaction between material properties, screw configuration, temperature, and processing conditions.
How Can the Optimal Screw Speed Be Determined?
USEON recommends conducting controlled trials to evaluate whether increasing screw speed provides measurable improvements.
A reliable evaluation should begin with stable operating conditions.
Important parameters to record include:
Material formulation and raw material characteristics
Screw configuration and feeding positions
Actual feeding rate and screw speed
Barrel temperature settings and actual melt temperature
Motor load and die pressure
Dispersion test results and final product properties
During initial trials, the formulation, feeding rate, and other controllable parameters should remain unchanged while screw speed is increased gradually.
Samples should only be collected after the process has stabilized.
Comparisons should be based on consistent testing methods, such as microscopic dispersion analysis, agglomerate size measurements, or appropriate filter pressure value (FPV) tests.
The objective is to identify whether the improvement in dispersion justifies any changes in melt temperature, energy input, or material properties.
What If Higher Screw Speed Does Not Improve Dispersion?
If increasing screw speed does not produce the desired results, other factors should be investigated.
These may include:
Material wetting and plasticization: Pigments and fillers must be adequately wetted before effective dispersive mixing can occur.
Feeding conditions: Unstable material feeding can lead to inconsistent mixing performance.
Screw configuration: The arrangement of conveying, kneading, and mixing elements can significantly influence dispersion efficiency.
Material formulation: Filler surface characteristics, polymer compatibility, and dispersing additives may also affect the final result.
In many cases, optimizing the screw configuration or material formulation may be more effective than simply increasing screw speed.
The Right Screw Speed Is Not Necessarily the Highest
The objective of twin-screw extrusion is not to operate at the maximum possible screw speed, but to identify conditions that deliver consistent product quality at the required production capacity.
An effective process must balance dispersion quality, melt temperature, material properties, and operating stability.
USEON's technical analysis emphasizes that screw speed should be evaluated as part of the overall extrusion process rather than as an independent solution to dispersion problems.
Polmak Plastik, working with USEON extrusion technologies, supports customers in selecting suitable extrusion systems and evaluating processing requirements for compounding, masterbatch, and other polymer applications.
Source: USEON Technology - Does Higher Screw Speed Improve Dispersion in a Twin-Screw Extruder? (November 7, 2026)
https://www.useon.com/know-how/twin-screw-extruder-screw-speed-dispersion/
NEWS ARCHIVE